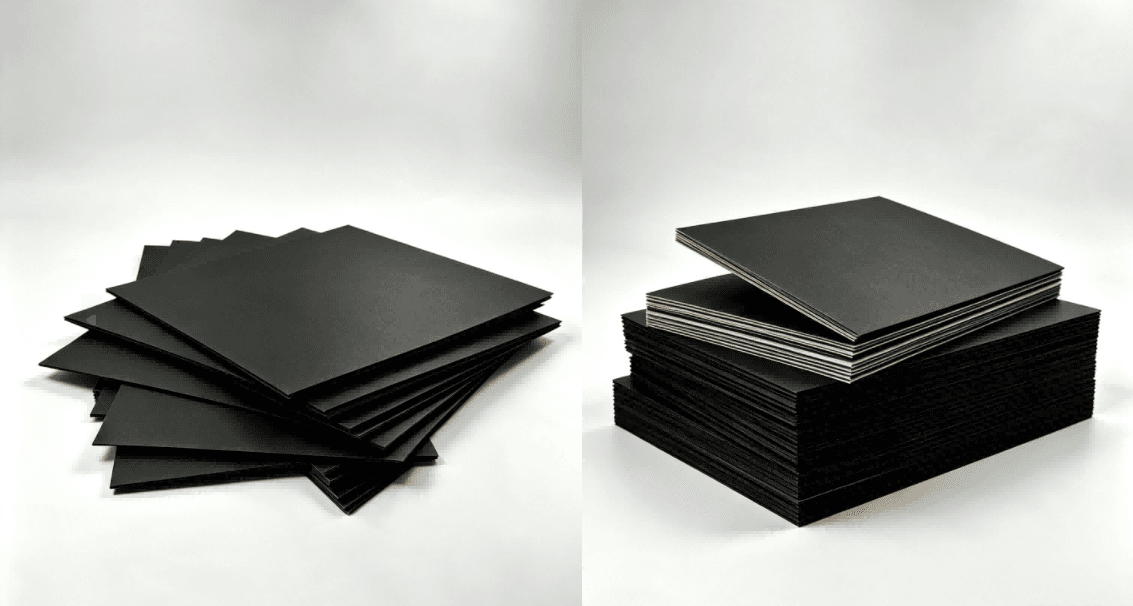
Black Paper Laminated Greyboard vs Black Paperboard: How Should Packaging Manufacturers Choose?
Black packaging paperboard is widely used in premium packaging applications due to its elegant appearance, stable performance, and excellent processing adaptability.
When selecting black packaging materials, packaging manufacturers usually compare two common solutions:
- Black Paper Laminated Greyboard
- Black Paperboard
Both materials can be produced with single-side black or double-side black structures. This article mainly compares the two double-side black paperboard solutions, focusing on differences in material structure, composition, thickness range, stiffness performance, processing characteristics, and application areas.
Understanding these differences helps packaging manufacturers select the right black paperboard material based on product design, production requirements, and cost targets.
What Is Black Paper Laminated Greyboard?
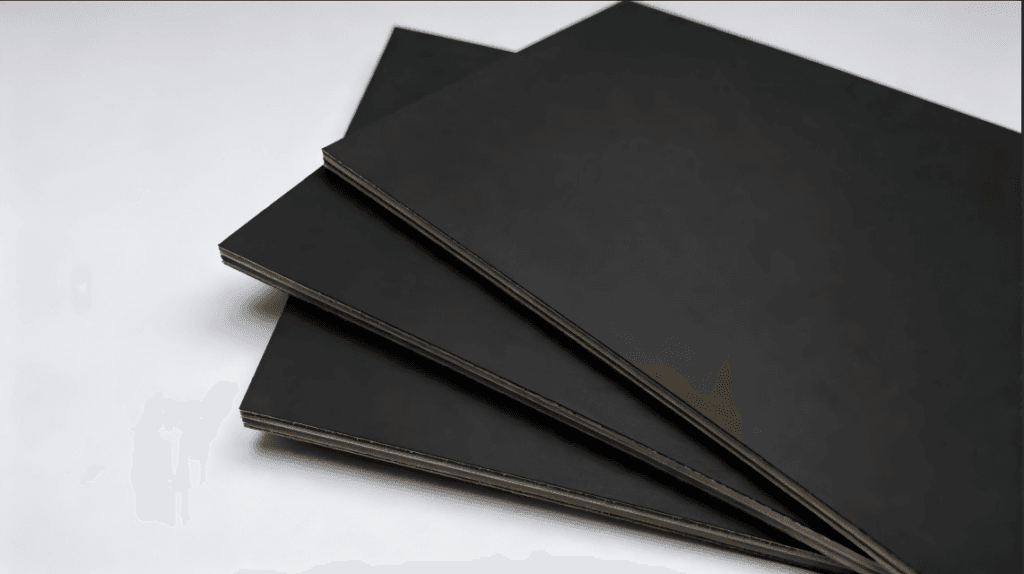
Black Paper Laminated Greyboard is a composite paperboard material made by laminating black paper onto a high-strength greyboard core.
Its main structure includes:
- Black paper surface layer: Provides a premium black appearance and surface finish.
- Greyboard core layer: Made from 100% recycled paper pulp, providing stable structural support.
This laminated structure combines the visual appeal of black paper with the structural performance of greyboard, offering:
- Stable dimensional performance;
- Good processing adaptability;
- Better cost efficiency.
Black Paper Laminated Greyboard typically has a thickness range of:
1.0–3.0mm
It is suitable for rigid packaging projects that require a balance between appearance, strength, and production stability.
What Is Black Paperboard?
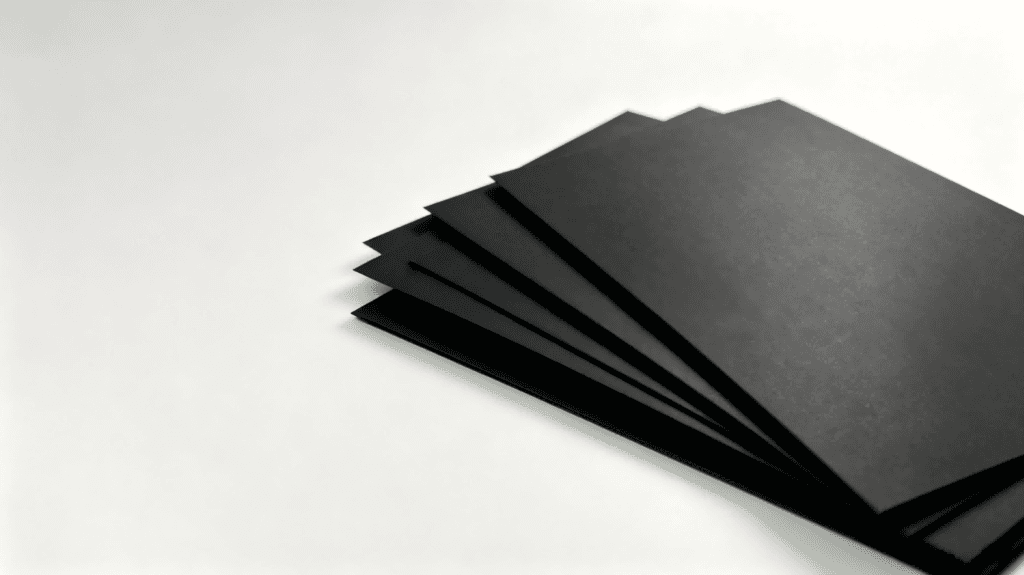
Black Paperboard is a fully black-colored paperboard with a consistent black appearance throughout the entire sheet.
Unlike laminated black greyboard, Black Paperboard is manufactured with black-colored fibers throughout the board structure, allowing the material to maintain a uniform black appearance from surface to interior.
Because the entire board has consistent coloration, Black Paperboard offers:
- Black appearance after cutting and die-cutting;
- No visible grey core exposure;
- Better visual consistency for premium products;
- Higher stiffness performance at the same thickness.
Double-side black Black Paperboard can reach a maximum thickness of approximately:
2.0mm
It is suitable for packaging and printed products that require black edges, refined processing, and a consistent premium appearance.
Key Differences Between Black Paper Laminated Greyboard and Black Paperboard
| Comparison Item | Black Paper Laminated Greyboard | Black Paperboard |
|---|---|---|
| Material Structure | Black paper laminated with greyboard core | Full black paperboard structure |
| Material Composition | Black paper + 100% recycled greyboard core | Black-colored fiber paperboard structure |
| Thickness Range | 1.0–3.0mm | Double-side black up to approximately 2.0mm |
| Cutting Edge Appearance | Grey core may become visible after cutting | Cutting edges remain black |
| Stiffness Performance | Stable structure, suitable for rigid packaging | Higher stiffness at the same thickness |
| Cost Advantage | Better cost efficiency for large-scale production | Relatively higher material cost |
| Main Applications | Gift boxes, rigid packaging, structural packaging | Hang tags, printed products, specialty black packaging |
Applications of Black Paper Laminated Greyboard
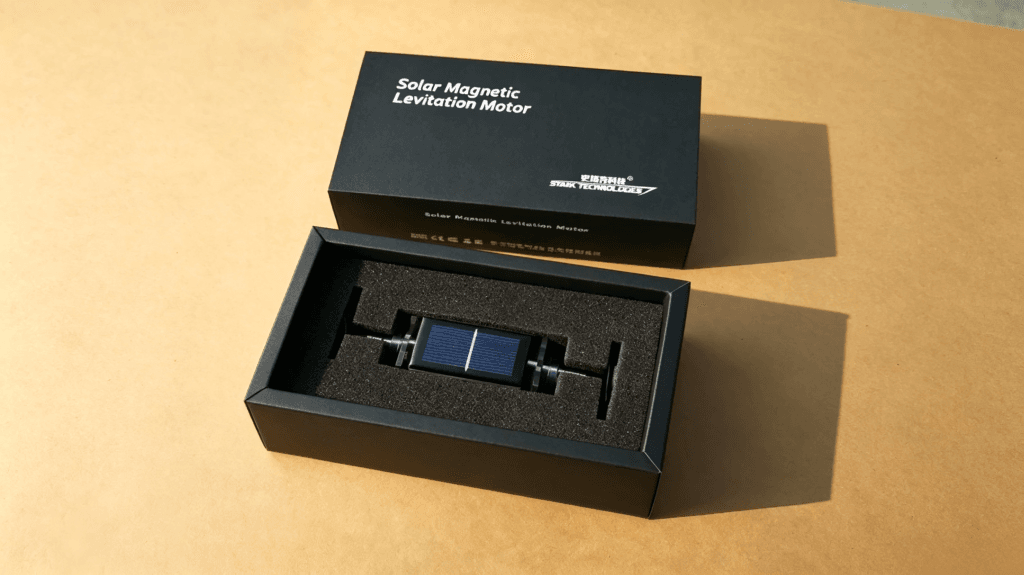
1. Luxury Gift Box Packaging
Black Paper Laminated Greyboard provides stable structural performance and is suitable for:
- Luxury gift boxes;
- Rigid gift packaging;
- Magnetic closure boxes;
- Premium retail packaging.
Its stable stiffness helps packaging maintain a strong three-dimensional structure and improve durability.
2. Cosmetic & Beauty Product Packaging
Cosmetic packaging requires both premium appearance and reliable structural performance.
Black Paper Laminated Greyboard is commonly used for:
- Cosmetic boxes;
- Beauty product packaging;
- Perfume packaging;
- Skincare gift boxes.
It also supports various finishing processes, including:
- Hot stamping;
- Embossing;
- Screen printing;
- UV coating.
3. Electronics Packaging
Electronics packaging requires good protection performance and dimensional stability.
Black Paper Laminated Greyboard is suitable for:
- Electronic product boxes;
- Display packaging;
- Internal support structures.
Its stable board performance meets the processing requirements of different packaging structures.
4. Board Game & Puzzle Packaging
Board game and puzzle packaging usually requires good structural stability and processing performance.
Black Paper Laminated Greyboard offers:
- Good stiffness;
- Stable die-cutting performance;
- Reliable structural support.
It is suitable for:
- Board game boxes;
- Puzzle boxes;
- Collector edition game packaging.
Applications of Black Paperboard
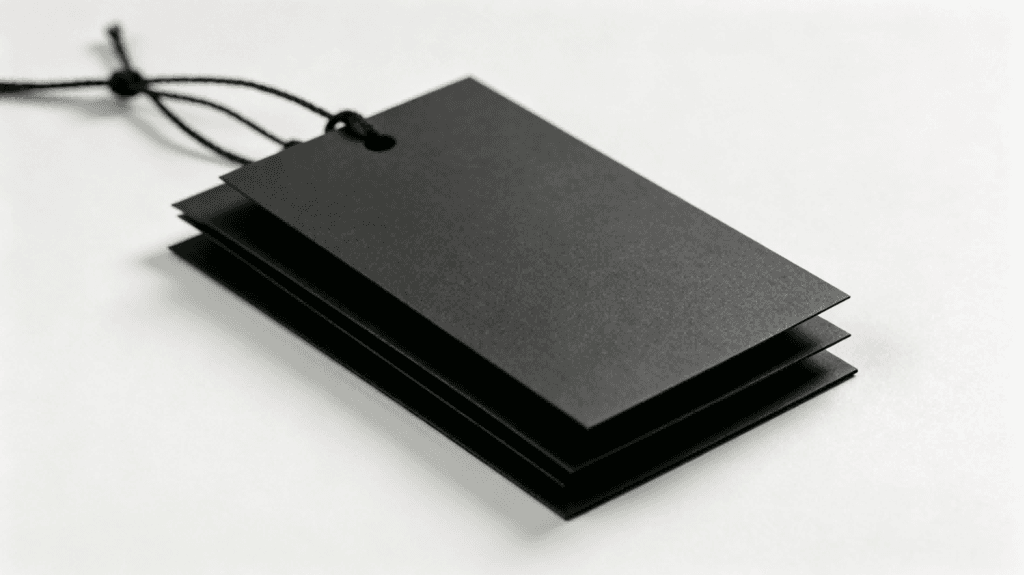
1. Hang Tags, Invitations & Premium Cards
Due to its consistent black appearance, Black Paperboard is suitable for:
- Fashion hang tags;
- Premium invitations;
- Luxury business cards;
- Brand promotional cards.
Its uniform black color enhances the premium visual experience of the product.
2. Double-Sided Visible Black Packaging
For packaging products that require the exterior, interior, and cutting edges to maintain the same black appearance:
Black Paperboard is suitable for:
- Double-side black rigid boxes;
- Jewelry boxes;
- Premium packaging structures.
Its full black structure helps avoid color differences during cutting and processing.
3. Art & Photography Background Applications
With its consistent black surface, Black Paperboard can be used as:
- Art background boards;
- Photography backgrounds;
- Product display boards.
4. Premium Hardcover & Specialty Packaging
Black Paperboard is suitable for:
- Premium hardcover products;
- Luxury book covers;
- Specialty black visual design applications.
How to Choose Between Black Paper Laminated Greyboard and Black Paperboard?
There is no absolute better choice between Black Paper Laminated Greyboard and Black Paperboard. The right option depends on the specific requirements of the packaging project.
If your project focuses on:
- Stable structural performance;
- Reliable large-scale production;
- Wider thickness options;
- Better cost efficiency;
Black Paper Laminated Greyboard is usually the better choice.
It provides a good balance between appearance, structural performance, and cost, making it suitable for most rigid packaging applications.
If your project focuses on:
- Black cutting edges;
- Consistent black appearance in exposed areas;
- Overall visual uniformity;
- Higher stiffness at the same thickness;
- Premium printing performance;
Black Paperboard is more suitable.
It is especially suitable for hang tags, invitations, premium cards, and products requiring a special black visual effect.
Hongtu Scenery Black Paperboard Solutions
As a professional black packaging paperboard manufacturer and supplier, Hongtu Scenery provides customized black paperboard solutions for global packaging manufacturers.
We supply:
- Black Paper Laminated Greyboard
- Solid Black Paperboard
- Full Black Paperboard
Based on different packaging requirements, we provide:
- Customized thickness options;
- Customized sheet sizes;
- Single-side black and double-side black structures;
- Material recommendations based on specific applications.
With stable production capabilities and extensive paperboard manufacturing experience, Hongtu Scenery helps customers select the right black packaging material according to their packaging design, processing requirements, and cost objectives.
Conclusion
Choosing the right black packaging paperboard is not only about appearance, but also about finding the right balance between visual requirements, structural performance, and production needs.
For packaging projects that require stable structure, flexible thickness options, and cost-efficient production, Black Paper Laminated Greyboard provides a practical solution for large-scale rigid packaging manufacturing.
For products that require a consistent black appearance, black cutting edges, and higher stiffness performance, Black Paperboard provides better performance for applications where visual quality and processing results are critical.
For packaging manufacturers, selecting the right material structure can reduce processing risks, improve production efficiency, and enhance the final product quality.
Hongtu Scenery provides professional material recommendations for different packaging applications, helping customers choose the most suitable black paperboard solution based on product design, processing methods, and market positioning.
Author Profile
-
HONGTUSCENERY is a professional manufacturer of composite paperboard,
providing sustainable and customized packaging solutions for global brands.
With nearly 20 years of industry experience, we focus on material performance,
structural strength, and green supply chain development.
Latest entries
 Double-Sided Kraft Laminated Greyboard2026-10-13Hidden Costs in Kraft Board Procurement: Why the Lowest Price Is Not Always the Best Deal
 Industry Insights2026-10-10How to Reduce Profit Losses from Paperboard Procurement Amid RMB Exchange Rate Fluctuations
 Company News2026-10-03Kraft Paperboard: Applications, Performance Advantages & Sustainability
 Double-Sided Kraft Laminated Greyboard2026-09-305 Key Factors for Choosing a Reliable Kraft Board for Packaging Supplier